• When Should You Add a Rosin Tackifier to Water-Based PSAs?
    When Should You Add a Rosin Tackifier to Water-Based PSAs?

    2026-09-30

    Low Initial Tack in Water-Based PSAs: When Should You Add a Rosin Tackifier Dispersion? A label lifts at the edges shortly after application. A tape bonds well to cardboard but peels easily from plastic packaging. When adhesive manufacturers encounter these problems, they need to check the substrate and processing conditions, as well as whether the formulation provides enough tack and peel strength. Water-based rosin tackifier dispersions are commonly used in water-based adhesives. When the base polymer forms a film properly but does not provide the required adhesion, a compatible tackifier dispersion can help adjust its performance. What Is the Difference Between Low Tack, Low Peel Strength, and Poor Holding Power? Customers may describe all three as “poor adhesion,” but each calls for a different approach. Problem Property to Check Role of the Tackifier Dispersion Labels lift immediately and require repeated pressing Initial tack A suitable tackifier can improve adhesion after brief contact Tape peels off easily after application Peel strength Can improve peel adhesion to the target substrate Labels or tape slip under a sustained load Holding power and cohesive strength Adding more tackifier alone may not solve the problem; the base polymer and overall formulation need to be checked Initial tack describes how readily the adhesive bonds after brief contact. Peel strength measures the force required to remove a label or tape. Holding power describes the adhesive’s ability to resist movement under a sustained load. Identifying which property is insufficient helps guide formulation changes. How Does a Water-Based Rosin Tackifier Dispersion Work? Water-based rosin tackifier dispersions are produced by dispersing rosin or modified rosin resin in water through an emulsification process. When blended with a compatible base polymer dispersion, they change the viscoelastic properties of the dried adhesive film, affecting its behavior during contact, bonding, and peeling. They are mainly used to improve tack and peel adhesion in self-adhesive labels, packaging tapes, and other water-based pressure-sensitive adhesives. Certain rosin ester dispersions are used to improve tack and peel adhesion to polyethylene and cardboard in acrylic and carboxylated SBR adhesive formulations. However, a tackifier cannot solve every bonding problem. Surface contamination, insufficient coating weight, or incomplete drying should be addressed first. When Should You Consider Adding One? One situation is when the adhesive forms a film properly, but labels do not stick readily after application and tack test results fall below requirements. Another is when the adhesive performs well on paper but provides insufficient peel strength on the customer’s plastic packaging. A third is when developing a new label or tape adhesive and the base polymer alone cannot provide the required tack. If the main problem is slippage under load, bond failure at elevated temperatures, or adhesive res...

    read more
  • Why Are Water-Based Resin Purchasing Costs Facing Upward Pressure?
    Why Are Water-Based Resin Purchasing Costs Facing Upward Pressure?

    2026-09-18

    Purchasing costs for water-based resins may rise as selected raw materials, energy and international transportation become more expensive. In September 2026, butyl acrylate prices moved higher in several markets. Some MDI suppliers also raised listed prices for selected products and regions. These materials are widely used in acrylic emulsions, pressure-sensitive adhesives and waterborne polyurethane dispersions. Transportation is adding further pressure. One global container freight index rose by approximately 9% over the past month, although changes varied significantly by route. Higher fuel costs, port congestion and disruption around major shipping routes may also increase freight, insurance and delivery expenses. For buyers, the impact is not limited to the resin quotation. The total landed cost may also include: Higher international freight charges Additional insurance or route-related costs Shorter quotation validity Longer or less predictable delivery times Extra inventory required to avoid production delays This does not mean that every water-based resin will increase by the same amount. The actual impact depends on the resin formulation, raw materials, destination and shipping route. Buyers planning large or time-sensitive orders should confirm the latest quotation, available stock, production schedule and freight cost. Earlier planning and closer communication with suppliers can help manage unexpected cost changes and delivery risks. Sinograce Chemical continues to monitor raw material and logistics conditions to provide customers with updated quotations, suitable resin recommendations and practical supply support. FAQ Are all water-based resin prices increasing? No. Price movements vary according to resin type, formulation, supplier and region. Why may the total purchasing cost increase? In addition to the product price, buyers may face higher freight, insurance, inventory and urgent-order costs. Which products may be more sensitive? Products that rely heavily on raw materials currently experiencing price or supply volatility may face greater cost pressure. What should buyers confirm before ordering? Buyers should check quotation validity, stock availability, production lead time, freight charges and expected delivery dates.

    read more
  • Which Is Better for Industrial Molds: PTFE or PFA Coating?
    Which Is Better for Industrial Molds: PTFE or PFA Coating?

    2026-09-10

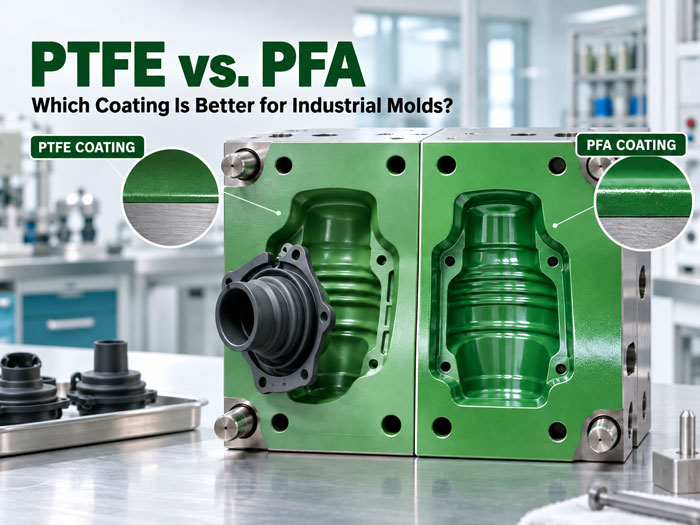
    Mold sticking is a common problem in plastic injection molding, rubber molding, and composite processing. Poor release may damage finished parts, increase mold-cleaning frequency, and interrupt production. PTFE and PFA coatings can both improve release, but their different processing characteristics make them suitable for different working conditions. The Main Difference Between PTFE and PFA PTFE has an extremely high melt viscosity. During sintering, its particles fuse to form a coating but do not flow like conventional thermoplastics. PFA is melt-processable, so it flows more readily during heating and can form a more continuous film. According to published resin data, PTFE has a typical melting peak of approximately 327°C, while PFA grades generally melt at 295–310°C. Both materials can provide continuous service temperatures of up to 260°C Property PTFE PFA Processing behavior Particles fuse during sintering but do not flow easily Melt-processable Typical melting point Approximately 327°C Approximately 295–310°C, depending on grade Continuous service temperature Up to 260°C Up to 260°C Release performance Extremely low friction and excellent release Excellent release with slightly higher friction Film structure Commonly used for thinner release coatings Better suited to thicker, more continuous coatings Cost Usually lower Usually higher Sinograce Chemical’s PF-609 and PFA-001 coatings also have a continuous service temperature of up to 260°C. This is the long-term operating limit rather than the curing temperature used during coating application. The values above provide a useful reference, but resin type alone does not determine the final result. Coating formulation, primer, film thickness, substrate preparation, and curing conditions also affect release, adhesion, and service life. When Is PTFE More Suitable? PTFE is generally preferred when low friction and clean release are the main requirements. It is well suited to industrial molds where a relatively thin coating is needed to preserve dimensions or fine surface details. For general mold-release applications, a water-based two-coat PTFE system, such as PTFE PF-609, can provide a low-friction release surface while keeping the coating relatively thin. PTFE also has excellent chemical resistance. However, when long-term corrosion protection depends on forming a thicker and more continuous barrier over the metal substrate, PFA may be more suitable. When Is PFA More Suitable? Since PFA flows during heating, it can form a thicker and more continuous fluoropolymer film. This makes it useful when the coating must provide both release and stronger isolation of the metal substrate. The difference becomes more relevant when molding PVC, fluororubber, halogen-containing compounds, or certain flame-retardant materials that may release corrosive substances during processing. PFA may also be considered when material erosion or repeated production cycles cause defects in a conventional release coating. ...

    read more
  • How PTFE + PFA Blending Helps Reduce Pinholes and Coating Peeling in Non-Stick Cookware
    How PTFE + PFA Blending Helps Reduce Pinholes and Coating Peeling in Non-Stick Cookware

    2026-09-03

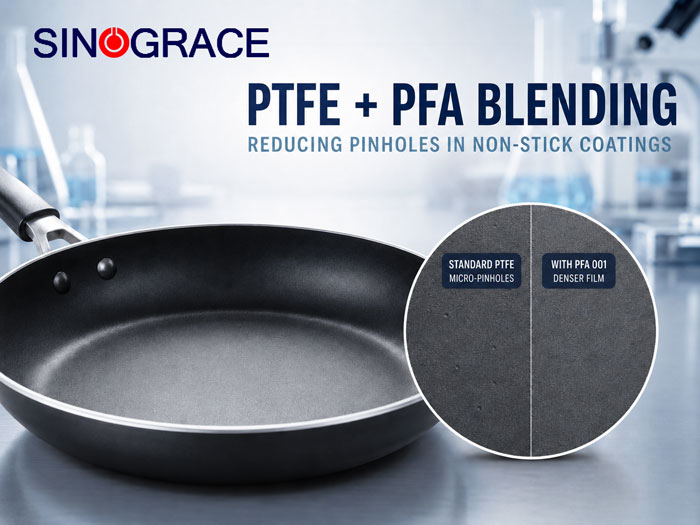
    In the non-stick cookware and bakeware industry, pinholes and premature coating peeling can reduce first-pass production yield and lead to customer returns. Both problems can be related to insufficient film density and microscopic porosity. Substrate preparation, coating thickness, and curing conditions may also affect the final result. 1. The Processing Limits of Pure PTFE Pure PTFE provides an extremely low coefficient of friction but has very limited melt flow at high temperatures. During sintering, PTFE melts and coalesces but does not flow like a conventional thermoplastic. As a result, microscopic voids may remain in the cured film. If these defects extend through the coating system, moisture, oils, and salts may reach the aluminum substrate, increasing the risk of corrosion, blistering, peeling, and declining non-stick performance. 2. PTFE + PFA Dispersion Blending Adding a melt-processable PFA dispersion can improve the flow behavior of a standard PTFE non-stick coating during curing. PFA 001  Modified Concentrated Dispersion melts at a lower temperature than standard PTFE. When used at a suitable dosage, it improves film consolidation and helps produce a smoother, denser coating without significantly increasing formulation costs. Performance Standard PTFE System With PFA 001 Practical Manufacturing Benefit Melt Behavior During Curing Very limited melt flow and leveling PFA adds a melt-flowing component Better leveling and film consolidation Melting Behavior PTFE melts at approximately 327°C PFA 001 melting point: 305 ± 10°C by DSC PFA begins melting earlier during curing Film Structure Microscopic voids may remain after sintering A denser and more uniform film can form Helps reduce pinholes and media penetration Cost Efficiency Lower resin cost, but surface defects may increase rework Dosage can be adjusted through formulation testing Fewer coating defects can improve first-pass yield and help offset the additive cost 3. Formulation and Handling PFA 001 is supplied as a waterborne dispersion with a typical solid content of 51% and a pH range of 8–10. It is suitable for use in many waterborne fluoropolymer formulations, although compatibility should be checked in the final coating system. Mixing: Stir gently and avoid high-speed mixing, excessive shear, and foaming. Storage: Store between 5°C and 30°C and protect from freezing. Gentle agitation at regular intervals can help reduce settling during extended storage. Safety: Refer to the latest SDS for complete handling and high-temperature processing information. Frequently Asked Questions 1. How does PFA 001 reduce pinholes in PTFE coatings? It improves melt flow during curing and helps the coating form a denser, more uniform film. 2. How much PFA 001 should be used? The dosage depends on the PTFE formulation, film thickness, and surface requirements. Contact us for a recommended starting dosage. 3. Is PFA 001 suitable for waterborne PTFE coatings? Yes. It is supplied as a waterborne ...

    read more

Copyright © 2015-2026 Anhui Sinograce Chemical Co., Ltd..All Rights Reserved.

top