Industry news

  • High-Tack Water-Based Pressure-Sensitive Adhesive for Film Labels
    High-Tack Water-Based Pressure-Sensitive Adhesive for Film Labels

    2026-04-08

    Sinograce Chemical’s high-tack water-based pressure-sensitive adhesive (PSA) is designed for PET, BOPP, PE and PVC film labels. It provides quick initial grab and strong peel adhesion. Its holding power helps reduce edge lift on curved surfaces and small-diameter containers. Contact us with your label film and container material to discuss a suitable adhesive grade.

    read more
  • How Do You Choose a Water-Based Acrylic Emulsion for Inks, Coatings, and Label Adhesives?
    How Do You Choose a Water-Based Acrylic Emulsion for Inks, Coatings, and Label Adhesives?

    2026-11-18

    What Is Water-Based Acrylic Emulsion Used For, and How Do You Choose a Grade? A water-based acrylic emulsion is a dispersion of acrylic polymer particles in water. It is commonly used as a binder in water-based printing inks, paper coatings, textile coatings, and some pressure-sensitive label adhesives. As the formulation dries, the polymer forms a film. To choose a grade, start with the substrate, processing conditions, and finished-product tests, then compare specifications such as solids content and viscosity. How the Application Changes the Selection Criteria For water-based ink printed on PVC edge banding, alcohol wipe resistance may be a requirement. Print the ink on the actual PVC, dry it under the intended production conditions, and check both ink adhesion and resistance to alcohol wiping. For a textile coating, the trial may instead focus on how the fabric feels after coating and whether the coating cracks when flexed. Application What to Check in a Trial Water-based printing inks Adhesion and rub resistance on the actual substrate. Check alcohol wipe resistance where required. Paper and paperboard coatings Wet rub resistance, sticking during stacking, and cracking at fold lines for folding cartons. Textile coatings and binders Fabric hand, flexibility, and wash resistance where required. Pressure-sensitive label adhesives Initial tack, peel strength, and holding power on the intended application surface. Frequently Asked Questions Can two acrylic emulsions with similar solids content be used interchangeably? Compare them in the same formulation, on the same substrate, and under the same drying conditions. Grades with similar solids content and viscosity can differ in film hardness, flexibility, and adhesion. Can an acrylic emulsion for water-based ink also be used for pigment grinding? Check the intended use of the grade. Some emulsions are designed primarily for film formation and adhesion. For pigment grinding, confirm the supplier recommends that use and evaluate viscosity and storage stability after grinding. If you are evaluating an acrylic binder for an ink, coating, or label adhesive, share your substrate, processing conditions, and target tests with Sinograce Chemical to discuss a grade for your trial.

    read more
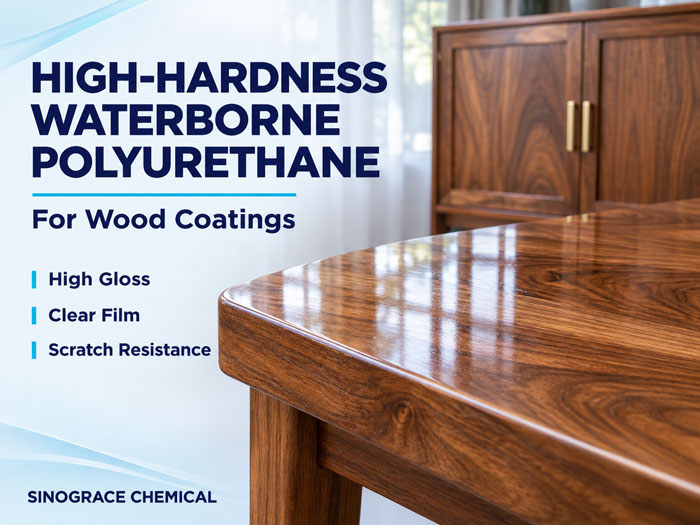
  • High-Hardness Waterborne Polyurethane Resins for Wood Coatings
    High-Hardness Waterborne Polyurethane Resins for Wood Coatings

    2026-11-09

    From Easily Marked Surfaces to More Durable Finishes: Sinograce High-Hardness Waterborne Polyurethane Resins A carefully sanded solid wood table or a cabinet door with precisely adjusted gloss and feel reflects a furniture manufacturer's attention to quality. Yet friction during handling or repeated wiping during everyday cleaning can leave marks on the finish. Even small scratches can affect appearance and create additional rework or after-sales demands. How can a wood finish combine an attractive appearance with durability? How can a waterborne formulation balance hardness, adhesion, and application performance? These questions make resin selection an important part of wood coating development. Sinograce Chemical's PU-108 waterborne polyurethane offers high hardness, high gloss, water resistance, and yellowing resistance for wood coating and clear varnish formulations. Its value for furniture and other wood products can be considered in three areas: surface protection, wood-grain appearance, and compatibility with the coating process. 1. Technical Performance: Building Protection into Wood Finishes Pencil Hardness of 2H–6H: A Foundation for Surface Protection Objects moving across a tabletop, repeated wiping of cabinet doors, and contact during furniture handling all test a coating's protective performance. PU-108 has a typical film pencil hardness range of 2H–6H, together with toughness, scratch resistance, and abrasion resistance. These properties provide a basis for developing high-hardness wood coatings. Product evaluation should also include scratch and abrasion testing to assess changes in the finish after friction. Hardness, toughness, surface slip, and degree of cure all influence performance in use. Actual hardness should be confirmed for the specific formulation and test conditions. 60° Gloss Above 90: Combining Protection with Wood-Grain Clarity Natural grain and color are important features of solid wood furniture. A clear coating's transparency, leveling, and gloss all influence how these details appear. PU-108 is an aliphatic polyurethane dispersion that dries to a clear film. It offers yellowing resistance, good leveling, and adhesion, with a 60° gloss value above 90. For high-gloss clear wood finishes, these properties help combine surface protection with the appearance of natural wood grain. Dry to Touch in 1–2 Hours at 25°C: Evaluating Drying Performance in Production A freshly coated test panel may already look smooth and attractive. A furniture component on the production line still has to pass through handling, assembly, stacking, and packaging. Each stage places different demands on the coating. PU-108 has a typical dry-to-touch time of 1–2 hours at 25°C, providing a reference for formulation development and drying-process evaluation. Production trials should also account for temperature, humidity, ventilation, coating application weight, and subsequent operations. After becoming dry to touch, the coating still requires fu...

    read more
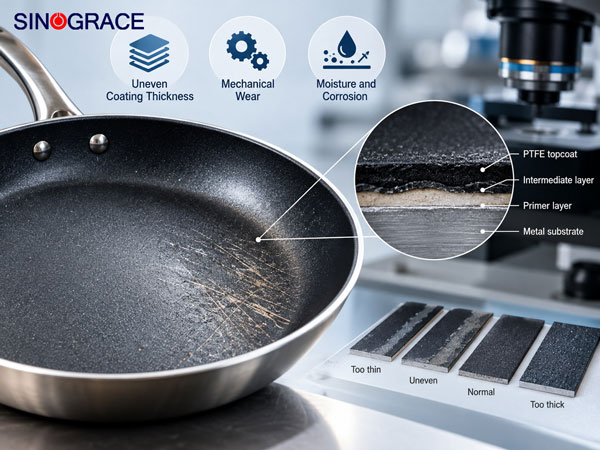
  • 2026 Study Reveals Key Factors Behind PTFE Non-Stick Coating Degradation
    2026 Study Reveals Key Factors Behind PTFE Non-Stick Coating Degradation

    2026-10-28

    Why Do PTFE Non-Stick Coatings Fail Prematurely? A 2026 Study on Thickness and Wear A cookware coating can pass initial adhesion testing yet gradually lose its food-release performance during use, even without visible peeling. A study published in theJournal of Failure Analysis and Preventionon March 30, 2026, examined the failure mechanisms of PTFE coatings on aluminized baking cookware. Through analysis of coating morphology, thickness variation, frictional wear and corrosion behavior, the researchers identified uneven film thickness and progressive material loss as important contributors to degradation in the tested system, rather than interfacial adhesion failure being the primary cause. How Wear and Uneven Thickness Affect PTFE Coatings The study found that areas with thinner coating coverage were more vulnerable to mechanical stress. Repeated friction caused material redistribution along the wear track, resulting in localized thinning and reduced surface protection. Changes in surface wettability may also facilitate the penetration of moisture and chloride ions, increasing the risk of corrosion beneath damaged coating regions. These mechanisms show how surface deterioration can affect coating performance without extensive separation from the substrate. The findings relate to a specific aluminized substrate and PTFE coating system and should not be considered a universal failure pattern for all non-stick cookware. Controlling Coating Thickness in Cookware Manufacturing In industrial production, coating uniformity depends on spray parameters, coating viscosity, substrate geometry and application conditions. Even when the average dry film thickness meets specifications, uneven deposition can leave vulnerable areas, particularly around edges and complex surfaces. For multilayer non-stick systems, each primer, intermediate layer and topcoat must be applied within its recommended thickness range. Excessive film build can complicate drying and sintering, while insufficient coverage may reduce local resistance to abrasion. Manufacturers should therefore monitor thickness distribution across the cookware surface rather than relying solely on average measurements or increasing the amount of coating applied. When Should the Primer Formulation Be Investigated? Heat-resistant binder resins such as polyamide-imide (PAI) and polyethersulfone (PES) are used in certain PTFE primer formulations to support adhesion to metal substrates. However, not every coating failure originates in the primer. Separation at the metal–primer interface may require examination of substrate cleaning, surface treatment and curing conditions. Delamination between coating layers calls for an investigation of interlayer compatibility and processing, while an intact primer beneath a worn topcoat suggests that surface durability and application conditions deserve closer attention. Identifying the location of failure before changing the formulation can prevent unnecessary adjustments ...

    read more

Copyright © 2015-2026 Anhui Sinograce Chemical Co., Ltd..All Rights Reserved.

top