• High-Hardness Waterborne Polyurethane Resins for Wood Coatings
    High-Hardness Waterborne Polyurethane Resins for Wood Coatings

    2026-11-09

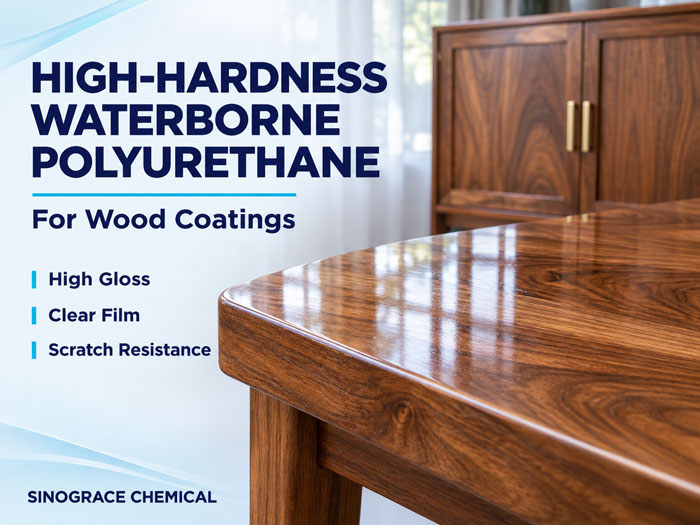
    From Easily Marked Surfaces to More Durable Finishes: Sinograce High-Hardness Waterborne Polyurethane Resins A carefully sanded solid wood table or a cabinet door with precisely adjusted gloss and feel reflects a furniture manufacturer's attention to quality. Yet friction during handling or repeated wiping during everyday cleaning can leave marks on the finish. Even small scratches can affect appearance and create additional rework or after-sales demands. How can a wood finish combine an attractive appearance with durability? How can a waterborne formulation balance hardness, adhesion, and application performance? These questions make resin selection an important part of wood coating development. Sinograce Chemical's PU-108 waterborne polyurethane offers high hardness, high gloss, water resistance, and yellowing resistance for wood coating and clear varnish formulations. Its value for furniture and other wood products can be considered in three areas: surface protection, wood-grain appearance, and compatibility with the coating process. 1. Technical Performance: Building Protection into Wood Finishes Pencil Hardness of 2H–6H: A Foundation for Surface Protection Objects moving across a tabletop, repeated wiping of cabinet doors, and contact during furniture handling all test a coating's protective performance. PU-108 has a typical film pencil hardness range of 2H–6H, together with toughness, scratch resistance, and abrasion resistance. These properties provide a basis for developing high-hardness wood coatings. Product evaluation should also include scratch and abrasion testing to assess changes in the finish after friction. Hardness, toughness, surface slip, and degree of cure all influence performance in use. Actual hardness should be confirmed for the specific formulation and test conditions. 60° Gloss Above 90: Combining Protection with Wood-Grain Clarity Natural grain and color are important features of solid wood furniture. A clear coating's transparency, leveling, and gloss all influence how these details appear. PU-108 is an aliphatic polyurethane dispersion that dries to a clear film. It offers yellowing resistance, good leveling, and adhesion, with a 60° gloss value above 90. For high-gloss clear wood finishes, these properties help combine surface protection with the appearance of natural wood grain. Dry to Touch in 1–2 Hours at 25°C: Evaluating Drying Performance in Production A freshly coated test panel may already look smooth and attractive. A furniture component on the production line still has to pass through handling, assembly, stacking, and packaging. Each stage places different demands on the coating. PU-108 has a typical dry-to-touch time of 1–2 hours at 25°C, providing a reference for formulation development and drying-process evaluation. Production trials should also account for temperature, humidity, ventilation, coating application weight, and subsequent operations. After becoming dry to touch, the coating still requires fu...

    read more
  • 2026 Study Reveals Key Factors Behind PTFE Non-Stick Coating Degradation
    2026 Study Reveals Key Factors Behind PTFE Non-Stick Coating Degradation

    2026-10-28

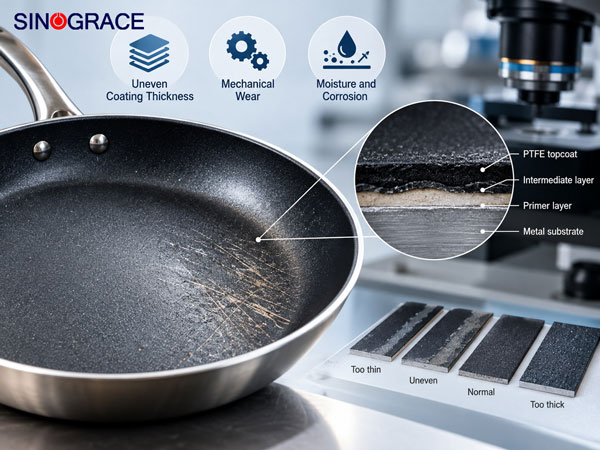
    Why Do PTFE Non-Stick Coatings Fail Prematurely? A 2026 Study on Thickness and Wear A cookware coating can pass initial adhesion testing yet gradually lose its food-release performance during use, even without visible peeling. A study published in theJournal of Failure Analysis and Preventionon March 30, 2026, examined the failure mechanisms of PTFE coatings on aluminized baking cookware. Through analysis of coating morphology, thickness variation, frictional wear and corrosion behavior, the researchers identified uneven film thickness and progressive material loss as important contributors to degradation in the tested system, rather than interfacial adhesion failure being the primary cause. How Wear and Uneven Thickness Affect PTFE Coatings The study found that areas with thinner coating coverage were more vulnerable to mechanical stress. Repeated friction caused material redistribution along the wear track, resulting in localized thinning and reduced surface protection. Changes in surface wettability may also facilitate the penetration of moisture and chloride ions, increasing the risk of corrosion beneath damaged coating regions. These mechanisms show how surface deterioration can affect coating performance without extensive separation from the substrate. The findings relate to a specific aluminized substrate and PTFE coating system and should not be considered a universal failure pattern for all non-stick cookware. Controlling Coating Thickness in Cookware Manufacturing In industrial production, coating uniformity depends on spray parameters, coating viscosity, substrate geometry and application conditions. Even when the average dry film thickness meets specifications, uneven deposition can leave vulnerable areas, particularly around edges and complex surfaces. For multilayer non-stick systems, each primer, intermediate layer and topcoat must be applied within its recommended thickness range. Excessive film build can complicate drying and sintering, while insufficient coverage may reduce local resistance to abrasion. Manufacturers should therefore monitor thickness distribution across the cookware surface rather than relying solely on average measurements or increasing the amount of coating applied. When Should the Primer Formulation Be Investigated? Heat-resistant binder resins such as polyamide-imide (PAI) and polyethersulfone (PES) are used in certain PTFE primer formulations to support adhesion to metal substrates. However, not every coating failure originates in the primer. Separation at the metal–primer interface may require examination of substrate cleaning, surface treatment and curing conditions. Delamination between coating layers calls for an investigation of interlayer compatibility and processing, while an intact primer beneath a worn topcoat suggests that surface durability and application conditions deserve closer attention. Identifying the location of failure before changing the formulation can prevent unnecessary adjustments ...

    read more
  • Meet Sinograce Chemical in Guangzhou During Canton Fair 2026
    Meet Sinograce Chemical in Guangzhou During Canton Fair 2026

    2026-10-19

    The discussions will cover four product areas: Water-based coatings and varnishes Customized coating solutions for specific applications Whether the project involves printing, textiles, cookware, bakeware or other industrial coating applications, the aim is to understand the production requirements and agree on practical next steps for product evaluation. Meeting dates October 22-24, 2026 Email sales@sinogracechem.com

    read more
  • Why Do Exterior Coatings Fail? | Sinograce Chemical
    Why Do Exterior Coatings Fail? | Sinograce Chemical

    2026-10-15

    Why Do Your Exterior Coatings Keep Failing? Are Your Binders and Additives Compatible? Uneven color in stone effect coatings, unwanted gelling during storage of multicolor paints, rain streaks on elastomeric finishes, and excessive aggregate loss during spraying—these problems can affect both coating quality and application efficiency. When trouble shooting, it is important to check how well the emulsion binder works with the additives in the formulation. Why Does Binder–Additive Compatibility Matter? The emulsion binder forms the coating film and influences adhesion, water resistance, and weathering performance. Additives are used in smaller amounts, but play essential roles in pigment dispersion, viscosity control, and foam management. These ingredients need to work together within the complete formulation to achieve consistent storage stability, application performance, and film properties. Four Common Problems—and What to Check 1. Patchy or uneven color Check pigment dispersion and compatibility between the binder and additives. In cool or humid conditions, pay particular attention to temperature, humidity, and drying time. 2. Excessive thickening during storage Poor interaction between the binder and thickening system can cause viscosity to rise during storage, making the coating difficult to apply. Tracking viscosity over time can help identify when the problem develops. 3. Rain streaks on the coating surface Rain exposure before the film has dried sufficiently can extract and redistribute water-soluble ingredients, leaving visible streaks. Both formulation composition and drying conditions should be evaluated. 4. Excessive spatter and aggregate loss Review the binder, thickening system, overall formulation, and spray settings together. Application trials are essential for confirming whether an adjustment improves performance. Published Research: Same Binder, Different Results A study published in PCI in 2021 compared three formulations made with the same binder. Films were dried at 25°C and 50% relative humidity, then evaluated for surfactant leaching. Surfactant leaching resistance ratings: 1–5, with 5 being best. Formulations using the same binder After 2 hours of drying After 4 hours After 24 hours Formulation 1 1 1 1 Formulation 2 5 5 5 Formulation 3 4 4 5 Source: Understanding Surfactant Leaching in Architectural Coatings*, Figure 13, PCI, 2021 Under these test conditions, the coatings showed different resistance to surfactant leaching despite using the same binder, highlighting the importance of evaluating the complete formulation. Three Steps to Selecting Binders and Additives Step 1: Start with the application. Stone effect coatings, multicolor paints, and elastomeric exterior paints have different requirements. Identify the main performance issue before selecting materials. Step 2: Check compatibility in the formulation. Keep a reference formulation and change one ingredient or dosage at a time. Compare viscosity, storage stabilit...

    read more
Copyright © 2015-2026 Anhui Sinograce Chemical Co., Ltd..All Rights Reserved.

top