• How PTFE + PFA Blending Helps Reduce Pinholes and Coating Peeling in Non-Stick Cookware
    How PTFE + PFA Blending Helps Reduce Pinholes and Coating Peeling in Non-Stick Cookware

    2026-09-03

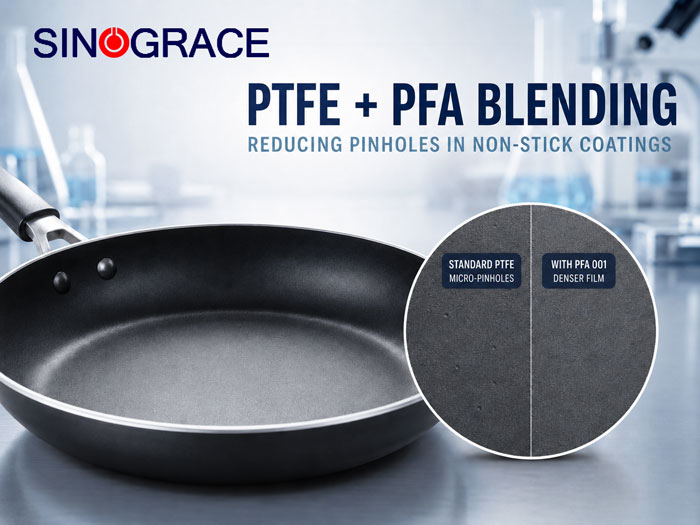
    In the non-stick cookware and bakeware industry, pinholes and premature coating peeling can reduce first-pass production yield and lead to customer returns. Both problems can be related to insufficient film density and microscopic porosity. Substrate preparation, coating thickness, and curing conditions may also affect the final result. 1. The Processing Limits of Pure PTFE Pure PTFE provides an extremely low coefficient of friction but has very limited melt flow at high temperatures. During sintering, PTFE melts and coalesces but does not flow like a conventional thermoplastic. As a result, microscopic voids may remain in the cured film. If these defects extend through the coating system, moisture, oils, and salts may reach the aluminum substrate, increasing the risk of corrosion, blistering, peeling, and declining non-stick performance. 2. PTFE + PFA Dispersion Blending Adding a melt-processable PFA dispersion can improve the flow behavior of a standard PTFE non-stick coating during curing. PFA 001  Modified Concentrated Dispersion melts at a lower temperature than standard PTFE. When used at a suitable dosage, it improves film consolidation and helps produce a smoother, denser coating without significantly increasing formulation costs. Performance Standard PTFE System With PFA 001 Practical Manufacturing Benefit Melt Behavior During Curing Very limited melt flow and leveling PFA adds a melt-flowing component Better leveling and film consolidation Melting Behavior PTFE melts at approximately 327°C PFA 001 melting point: 305 ± 10°C by DSC PFA begins melting earlier during curing Film Structure Microscopic voids may remain after sintering A denser and more uniform film can form Helps reduce pinholes and media penetration Cost Efficiency Lower resin cost, but surface defects may increase rework Dosage can be adjusted through formulation testing Fewer coating defects can improve first-pass yield and help offset the additive cost 3. Formulation and Handling PFA 001 is supplied as a waterborne dispersion with a typical solid content of 51% and a pH range of 8–10. It is suitable for use in many waterborne fluoropolymer formulations, although compatibility should be checked in the final coating system. Mixing: Stir gently and avoid high-speed mixing, excessive shear, and foaming. Storage: Store between 5°C and 30°C and protect from freezing. Gentle agitation at regular intervals can help reduce settling during extended storage. Safety: Refer to the latest SDS for complete handling and high-temperature processing information. Frequently Asked Questions 1. How does PFA 001 reduce pinholes in PTFE coatings? It improves melt flow during curing and helps the coating form a denser, more uniform film. 2. How much PFA 001 should be used? The dosage depends on the PTFE formulation, film thickness, and surface requirements. Contact us for a recommended starting dosage. 3. Is PFA 001 suitable for waterborne PTFE coatings? Yes. It is supplied as a waterborne ...

    read more
  • Why Does Ink Shrink or Leave Bare Spots on PP, PE and PET Films?
    Why Does Ink Shrink or Leave Bare Spots on PP, PE and PET Films?

    2026-08-27

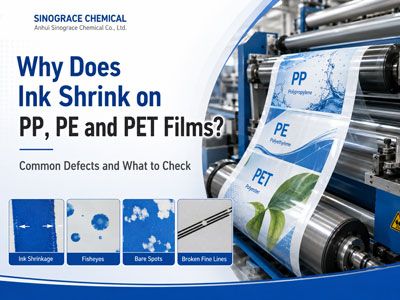
    A few missing dots or broken fine lines may not look serious during a short printing trial. Once the line returns to normal production speed, the same film may start showing bare spots, uneven solid areas or incomplete small text. When this happens, the ink is often adjusted first. But the defect may also come from the film condition or from the way the ink and substrate work together. The Defect Usually Gives the First Clue Poor wetting does not always affect the whole printed area. It often appears first in areas that leave little room for variation: Fine lines become broken Small characters lose definition Solid areas develop isolated bare spots Ink pulls back shortly after transfer Fisheyes appear in local areas Defects increase as line speed rises If the print looks acceptable at low speed but changes during production, it is worth checking more than the ink viscosity alone. The film being used on the machine, the pretreatment condition and the actual defect pattern can all help narrow down the cause. PP, PE and PET Need Different Treatment Plastic films may look similar, but they do not behave the same way during printing. PP and PE normally need more attention before printing. A clean-looking film can still give uneven ink coverage if its printable surface is not in the right condition. PET behaves differently and uses a different primer approach. If the film has already been corona treated, the material currently running on the press should still be checked rather than assuming that an earlier treatment record represents its present printing condition. For production troubleshooting, the actual print result is more useful than treating PP, PE and PET as one group. Primer Selection Starts With the Film Primer selection should follow the substrate and the printing system, not just solids, viscosity or appearance. For corona-treated PE, PP, OPP and BOPP, Anhui Sinograce Chemical offers SA-248G, a water-based modified acrylic printing top coating. Typical data: Solid content: 40±1% pH: 6.0–8.0 Viscosity at 25℃: 100–200 mPa·s Tg: 30℃ SA-248G is designed for good leveling and adaptability to UV ink printing. For applications with additional surface-performance requirements, it also provides high gloss, water resistance and scratch resistance. For corona-treated PET/BOPET, SA-235 uses a different modified acrylic system. Typical data: Solid content: 35±1% pH: 7.0–8.0 Viscosity at 25℃: 100–200 mPa·s Tg: 28℃ SA-235 is designed for PET / BOPET UV printing, with good ink acceptance and leveling. The two products have similar viscosity ranges, but they are intended for different film surfaces. Similar numbers on a technical data sheet do not make the products interchangeable. Checks to Make on the Printing Line Before making a major change to the ink formulation, compare the actual production conditions: Film type Pretreatment condition Location and shape of the printing defect Trial speed and normal production speed Ink viscosity and surface tension...

    read more
  • What Is Driving the Shift to Water-Borne Adhesives in Hot Stamping Foil Production?
    What Is Driving the Shift to Water-Borne Adhesives in Hot Stamping Foil Production?

    2026-08-21

    Hot stamping is widely used to add metallic and decorative effects to packaging, labels, paper, plastic films, and synthetic leather. For many years, solvent-based adhesives have been the standard choice for this process. That is beginning to change. Foil manufacturers are paying more attention to VOC emissions, solvent handling, workplace safety, and customer requirements for more sustainable materials. As a result, water-borne polyurethane adhesives are becoming a practical option for hot stamping foil production. Water is used as the main carrier in these adhesives, which can reduce the use of conventional organic solvents. This does not mean that every water-borne product is solvent-free, so the actual VOC content should always be checked in the relevant technical and safety documents. Processing performance is just as important as environmental considerations. A hot stamping adhesive must dry properly on the coating line, remain non-tacky during rewinding and storage, and activate at the required stamping temperature. Some modified polyurethane adhesives can be used at 95–135°C. This lower activation range is useful for papers and plastic films that may deform under excessive heat. The actual stamping temperature will still depend on the substrate, foil structure, pressure, speed, and equipment. Drying also needs to be assessed under real production conditions. Coating weight, oven temperature, airflow, and line speed all affect the final result. Sinograce Chemical manufactures water-borne adhesives for hot stamping foil production. Our PU-8441 is designed for fast drying, good anti-back-tack performance, heat resistance, and adhesion to paper, OPP, PET, PVC, leather, and other substrates. Drying also needs to be assessed under actual production conditions, as coating weight, oven temperature, airflow, and line speed can all affect the result. For foil manufacturers considering this transition, selecting an adhesive that matches both the substrate and the existing coating process is essential. Sinograce Chemical develops water-borne adhesive solutions for hot stamping foil production, including PU-8441, a modified polyurethane adhesive suitable for paper, OPP, PET, PVC, leather, and other substrates. FAQ Why are manufacturers considering water-borne hot stamping adhesives? The main reasons are lower dependence on organic solvents, VOC control, safer solvent handling, and growing demand for more sustainable production. Can a water-borne adhesive dry fast enough on a coating line? Yes, a suitable formulation can provide fast drying. The actual result depends on coating weight, oven settings, airflow, and line speed. What is the benefit of low-temperature activation? It can reduce heat exposure for sensitive papers and films and provide more flexibility when setting the stamping process.

    read more
  • From DMF-Based Systems to Waterborne Polyurethane: The Low-VOC Transition in Industrial Glove Coatings
    From DMF-Based Systems to Waterborne Polyurethane: The Low-VOC Transition in Industrial Glove Coatings

    2026-08-12

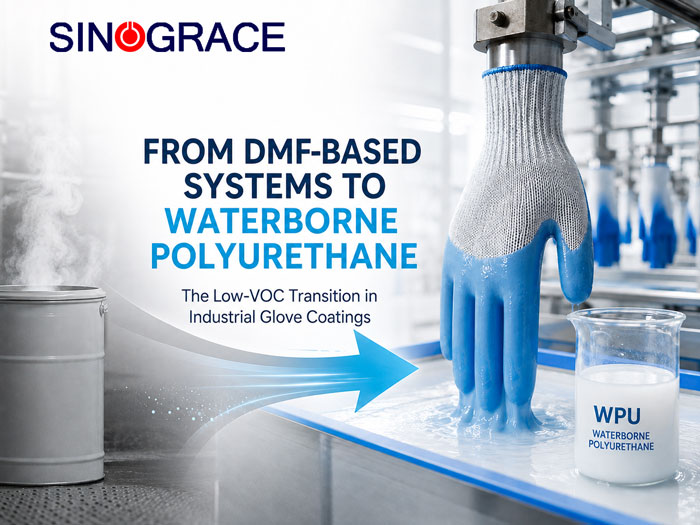
    Introduction As glove manufacturers worldwide pay increasing attention to worker health, VOC emissions, and chemical management in finished products, traditional solvent-based polyurethane glove coatings that rely on solvents such as DMF are facing increasingly stringent environmental and health compliance requirements. Against this background, low-VOC waterborne polyurethane (WPU) coatings that can be used in DMF-free formulations are becoming an important technical direction for industrial glove coatings. 1. Green Transition: From Solvent-Based Systems to Waterborne Polyurethane Reducing Dependence on Traditional Solvents Waterborne polyurethane uses water as its primary dispersion medium. It can significantly reduce the use and evaporation of organic solvents during coating production and application, helping to lower VOC emissions and reduce dependence on traditional DMF-based systems. Improving the Production Environment The use of low-VOC water-based systems helps reduce the use and evaporation of organic solvents during production, improve the working environment in glove manufacturing facilities, and reduce the pressure associated with solvent storage, handling, and occupational exposure management 2. Balancing Technology and Performance in Waterborne PU Glove Coatings In the past, the industry generally focused on the abrasion resistance, grip performance, and drying efficiency of water-based coatings. With advances in new-generation waterborne polyurethane resin synthesis technology, some mature systems can now achieve a good balance among the following properties and meet the basic requirements of industrial glove coatings. Mechanical and Abrasion-Resistance Performance By optimizing the molecular structure and degree of crosslinking of waterborne polyurethane, the tensile strength, abrasion resistance, and durability of the coating can be improved. Final performance is also affected by the coating formulation, coating thickness, substrate type, and drying conditions. Therefore, testing under actual application conditions is necessary. Grip and Flexible Hand Feel Through the coordinated design of the resin structure, coating formulation, and surface treatment process, the required dry and wet grip performance can be achieved while maintaining the softness and fit of the gloves. Because grip performance is also related to the coating surface structure, formulation additives, and processing conditions, resin selection should be comprehensively evaluated based on the actual use environment of the gloves. Process Compatibility Waterborne PU resins and their formulations can be adjusted according to the glove substrate, dipping method, coagulation process, and drying conditions to meet the process requirements of different glove production lines. When changing from a traditional DMF-based system to a water-based system, it is generally necessary to test and optimize the formulation viscosity, coating amount, drying temperature, and producti...

    read more

Copyright © 2015-2026 Anhui Sinograce Chemical Co., Ltd..All Rights Reserved.

top